OEE (Overall Equipment Effectiveness) is one of the most widely used manufacturing KPIs for measuring the actual efficiency of production processes.
By using this KPI, production managers can determine how much time their equipment is producing, how efficiently machines are operating, and what percentage of output meets quality standards.
Its widespread adoption has made OEE a benchmark metric within methodologies such as Lean Manufacturing, as it helps identify production losses, prioritize improvement initiatives, and objectively measure their impact.
However, calculating OEE correctly involves much more than applying a mathematical formula. To make this metric truly valuable, it is essential to understand exactly what it measures, how to interpret the results, and how to use the insights gained to drive continuous improvement.
Although OEE can be calculated manually, many manufacturers automate data collection through MES software to monitor Overall Equipment Effectiveness in real time.
In this article, you’ll gain a complete understanding of OEE: what it means, how to calculate it, its three core components, what constitutes a good OEE score, how to start using it in a manufacturing environment, and why more and more companies are automating OEE measurement with MES software such as Mapex.
What is OEE?
OEE is a manufacturing performance metric used to measure the overall effectiveness of a machine, production line, or manufacturing plant.
Its purpose is to show what percentage of planned production time is actually converted into productive manufacturing, based on three key factors:
- Equipment availability.
- Production at the planned operating speed.
- The percentage of manufactured parts that meet quality standards.
In other words, OEE answers a simple but critical question: What percentage of our theoretical production capacity are we actually utilizing?
For this reason, OEE does not simply measure how much a machine produces. It measures how efficiently the equipment performs throughout the entire production process.
This comprehensive view helps manufacturers identify improvement opportunities that would often go unnoticed if they only tracked isolated metrics such as the number of parts produced or machine operating hours.
What does OEE stand for?
OEE stands for Overall Equipment Effectiveness, a manufacturing KPI used to measure how effectively a machine, production line, or manufacturing operation performs.
Although the term is sometimes translated into other languages as Global Equipment Efficiency or Overall Equipment Efficiency, Overall Equipment Effectiveness is the standard terminology used across the manufacturing industry.
The concept of effectiveness best reflects the purpose of this metric because it combines three key dimensions of production performance: Availability, Performance, and Quality.
Rather than measuring output alone, OEE quantifies all the production losses that prevent equipment from reaching its maximum potential.
For this reason, OEE has become one of the most widely used KPIs for evaluating operational efficiency in manufacturing environments.
What is OEE used for?
More than just a KPI, OEE is a management tool that helps manufacturers understand how efficiently a production process is actually performing.
By calculating OEE on a regular basis, companies can identify where the biggest efficiency losses occur and determine which improvement opportunities should be prioritized first.
Some of the main applications of OEE include:
- Identifying production bottlenecks.
- Prioritizing continuous improvement initiatives.
- Comparing performance across machines, production lines, or manufacturing plants.
- Evaluating the impact of process improvement projects.
- Tracking efficiency trends over time.
- Supporting data-driven decision-making.
In addition, OEE provides a common performance framework for production, maintenance, and quality teams. By using the same metric, departments can align their efforts, collaborate more effectively, and focus on improving overall manufacturing performance.
OEE vs. efficiency vs. productivity: what’s the difference?
Although the terms are often used interchangeably, efficiency and productivity are not the same.
Productivity measures how much output is produced over a given period of time, while efficiency evaluates how effectively available resources are used to achieve that output.
For example, a manufacturing plant can increase production simply by adding extra shifts or installing more equipment. However, that does not necessarily mean the operation has become more efficient.
This is where OEE provides valuable insight. It measures how much of the available production capacity is actually being utilized, taking into account equipment availability, performance, and quality.
For this reason, many manufacturers use OEE alongside other production KPIs to gain a more comprehensive view of overall plant performance.
How is OEE calculated?
The OEE calculation is based on three core metrics that represent the primary sources of production losses in any manufacturing process.
Each metric evaluates a different aspect of equipment performance. Together, they provide an accurate picture of overall manufacturing efficiency.
The three components of OEE are:
- Availability, which measures how much of the planned production time the equipment was actually running.
- Performance, which evaluates whether production is operating at the expected speed.
- Quality, which measures the percentage of manufactured products that meet the required quality standards.
Analyzing these three factors separately is especially valuable because it allows manufacturers to quickly identify where production capacity is being lost and prioritize the most effective improvement actions.
Availability
Availability measures the amount of time a machine is actually producing compared to the total planned production time.
It is calculated using the following formula: Availability = Run Time / Planned Production Time
This calculation excludes periods when production was not scheduled, such as public holidays, planned shutdowns, or preventive maintenance.
When availability decreases, the root cause is typically unplanned downtime, equipment failures, lengthy changeovers, material shortages, or other unexpected production stoppages. For this reason, it is important to monitor maintenance KPIs such as MTBF (Mean Time Between Failures) and MTTR (Mean Time to Repair).
Performance
Performance measures whether equipment is operating at its designed production speed.
Even if a machine runs throughout an entire shift, it may still produce below its ideal cycle rate due to minor stops or reduced operating speeds.
It is calculated as: Performance = Actual Output / Theoretical Expected Output
Performance losses are typically caused by micro-stoppages, reduced operating speeds, or other small inefficiencies that may seem insignificant individually but can have a substantial impact on overall productivity.
Quality
The third component of OEE measures the percentage of production that meets the required quality standards.
Its formula is: Quality = Good Units Produced / Total Units Produced
This metric captures losses resulting from defective parts, rejected products, rework, and production scrap.
The higher the percentage of conforming products, the greater the contribution of the Quality factor to the overall OEE score.
For a practical explanation of how the three OEE components work together, watch this video:
OEE formula
Once the three core components have been calculated, OEE is determined by multiplying them together: OEE = Availability × Performance × Quality
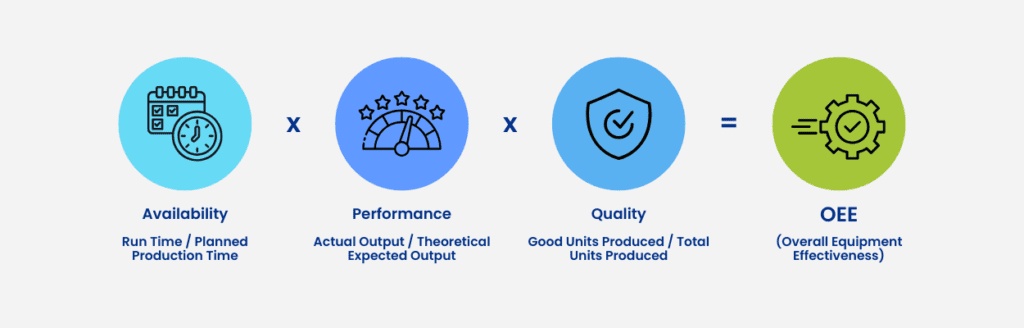
The result is expressed as a percentage and represents the overall efficiency of the production process during the planned production time.
For example, if a production line achieves 90% Availability, 95% Performance, and 98% Quality, the resulting OEE is 83.8%.
This calculation demonstrates how even relatively small losses in each component can significantly reduce overall manufacturing efficiency.
OEE can also be expressed using a simplified formula: OEE = Fully Productive Time / Planned Production Time
Both formulas produce the same result. However, calculating OEE by breaking it down into its three components makes it much easier to identify which factor is limiting production performance.
What is a good OEE score?
Interpreting the result correctly is just as important as calculating the metric itself.
An OEE score of 70% may represent excellent performance in some manufacturing processes, while in highly automated production environments it could indicate significant room for improvement.
As a general benchmark, the following OEE classification is widely used:
| OEE Value | Interpretation |
|---|---|
| Less than 60% | Low efficiency level. There are significant opportunities for improvement. |
| Between 60% and 75% | Acceptable performance, although there are still significant losses that can be reduced. |
| Between 75% and 85% | Good operational performance. |
| More than 85% | Excellent performance associated with World Class Manufacturing. |
However, these benchmarks should always be interpreted within the context of the specific industry, the type of manufacturing process, and the level of automation in the facility.
Rather than aiming for a specific percentage, the primary purpose of OEE is to provide a reliable benchmark for continuous improvement and to measure the impact of improvement initiatives over time.
What reduces this KPI? The Six Big Losses of OEE
When an OEE score falls below expectations, it indicates that production losses are limiting the equipment’s productive capacity.
These losses do not occur randomly. In Lean Manufacturing and Total Productive Maintenance (TPM), they are traditionally grouped into the Six Big Losses of OEE—a framework that helps manufacturers identify whether efficiency is being reduced by losses in Availability, Performance, or Quality.
In general, these losses can be grouped into three main categories:
| OEE Component | Main Losses |
|---|---|
| Availability | Breakdowns and setup or changeover time. |
| Performance | Minor stops and reduced operating speed. |
| Quality | Defects, rework, and startup losses. |
This classification makes it easier to prioritize improvement initiatives by focusing efforts on the type of loss that has the greatest impact on production performance.
Not all manufacturing plants face the same challenges. In some facilities, equipment failures are the primary source of losses, while in others, the biggest issues stem from lengthy changeovers, reduced operating speeds, or quality defects.
Understanding the Six Big Losses of OEE is the first step toward achieving sustainable improvements in manufacturing efficiency.
How to improve OEE
Once the root causes of production losses have been identified, the next step is to address them.
Improving OEE is not about increasing a single percentage in isolation. Instead, it involves systematically reducing the inefficiencies that affect Availability, Performance, and Quality.
In practice, this typically means implementing initiatives such as reducing equipment failures, optimizing changeover times, minimizing minor stops, improving quality control, and using reliable production data to make faster, better-informed decisions.
Every manufacturing operation has a different starting point, so there is no universal strategy for improving OEE. The key is to identify which of the three OEE components is underperforming and prioritize the actions that will deliver the greatest impact.
Methodologies such as Total Productive Maintenance (TPM), SMED (Single-Minute Exchange of Die), Root Cause Analysis (RCA), and Statistical Process Control (SPC) are commonly used to support OEE improvement initiatives. However, they should always be applied according to the specific needs of each manufacturing operation.
For a more in-depth guide, read our article on how to improve OEE and maximize manufacturing efficiency, where we explore proven strategies for increasing Availability, Performance, and Quality over the long term.
How to implement OEE in a manufacturing plant
Calculating OEE occasionally is relatively straightforward. The real challenge is turning it into a routine management tool for continuous improvement.
Implementing OEE involves defining which machines or production lines will be monitored, establishing standardized criteria for data collection, ensuring data accuracy, and creating a consistent methodology for analyzing performance.
Many manufacturers begin by monitoring a single machine or pilot production line before expanding OEE measurement across the entire facility. This phased approach allows them to validate the data collection system, refine operating procedures, and build confidence in the metric before scaling the project.
Beyond the technology itself, successful OEE implementation depends on ensuring that production, maintenance, and quality teams use the same measurement criteria and performance analysis standards.
If you’re planning to introduce OEE in your facility, check out our step-by-step guide on how to implement OEE in a manufacturing plant, where we explain the typical implementation stages and share best practices for collecting reliable production data from day one.
The role of operators in OEE success
Although automated data collection is becoming increasingly common, people continue to play a critical role in ensuring that OEE accurately reflects what is happening on the shop floor.
Operators have first-hand knowledge of how equipment performs and, in many cases, are responsible for validating production events, classifying certain types of downtime, and identifying improvement opportunities before any automated system can detect them.
For this reason, OEE should not be presented as a tool for evaluating individual employee performance. Instead, it should be positioned as a manufacturing KPI that helps improve production processes.
When operators understand what is being measured and why it matters, the quality of the recorded data improves significantly, making it much easier to build and sustain a culture of continuous improvement.
For practical recommendations, read our guide on how to engage operators to ensure OEE success, where you’ll find strategies for communicating the initiative, reducing resistance to change, and encouraging participation across the organization.
How to measure OEE automatically
Many manufacturers begin by calculating OEE using spreadsheets or manual production records.
While this approach may be sufficient during the early stages, it becomes increasingly difficult to maintain accurate and reliable data as the number of machines grows or production processes become more complex.
Manual data collection is time-consuming, increases the risk of errors, and makes real-time performance monitoring much more challenging.
For this reason, an increasing number of manufacturers automate OEE measurement with a Manufacturing Execution System (MES). An MES collects production data directly from machines and transforms it into actionable performance metrics that support faster, data-driven decision-making.

The main benefits of automated OEE measurement include:
- Greater data accuracy and reliability.
- Real-time OEE monitoring.
- Reduced administrative workload.
- Immediate detection of production deviations.
- Performance dashboards for visualizing key manufacturing KPIs.
- Integration with other production and quality metrics.
Rather than simply calculating a percentage, an MES system turns OEE into an operational management tool that helps manufacturers identify problems before they impact productivity.
Real-world OEE improvement success stories
Continuously measuring OEE does more than provide an efficiency score. It enables manufacturers to identify exactly which production losses are affecting performance and take targeted action to eliminate them.
When data collection is automated and OEE analysis becomes part of day-to-day production management, the metric evolves from a simple KPI into a powerful continuous improvement tool.
One example is Aciturri, an aerospace manufacturer that increased OEE by 10 percentage points across a group of machines at its Ircio facility after analyzing machine downtime data collected by Mapex.
As Diego Pinacho, the company’s Digitalization Manager, explains: “In 2018, by analyzing the downtime information provided by Mapex, we increased OEE by 10 percentage points across a group of machines at our Ircio plant. Without a digitalized OEE system, it would have been extremely difficult to identify the root causes of downtime and implement the appropriate continuous improvement actions.”
Another example is Solera, which calculated OEE using spreadsheets for an entire year before implementing MapexPM to automate data collection and evaluate the impact of mold changeovers on productivity.
With access to real-time production data, the company improved its OEE by more than five percentage points, as confirmed by its Plant Manager: “The positive impact of Mapex has been particularly noticeable in the Production department, where OEE has increased by more than five percentage points.”
If you’d like to learn how to achieve similar results in your own facility, contact our team.
FAQs about OEE
Can OEE be higher than 100%?
No. The maximum possible OEE score is 100%, representing the ideal manufacturing scenario in which equipment runs for all planned production time, operates at its ideal speed, and produces only defect-free products.
Can OEE be calculated manually?
Yes. OEE can be calculated manually using the formulas for Availability, Performance, and Quality. However, as production data volumes increase, manual data collection becomes increasingly inefficient and significantly raises the risk of calculation errors.
How often should OEE be measured?
The optimal measurement frequency depends on the manufacturing process and business objectives. Many companies monitor OEE per shift, while others track it in real time to detect production issues and respond more quickly.
Can OEE be used in any industry?
Yes. Although OEE originated in the manufacturing sector, it is now widely used across industries including food and beverage, automotive, plastics, metalworking, consumer goods manufacturing, and many other industrial sectors.